OEM/ODM Outdoor Hiking Backpack Designed for Your Brand
Fully integrated hiking backpack manufacturing. Osgoodway manage every step—from technical sampling to final assembly—to ensure stable, reinforced structures that excel in real-world outdoor environments. Precision-engineered. Trail-ready. Built to endure
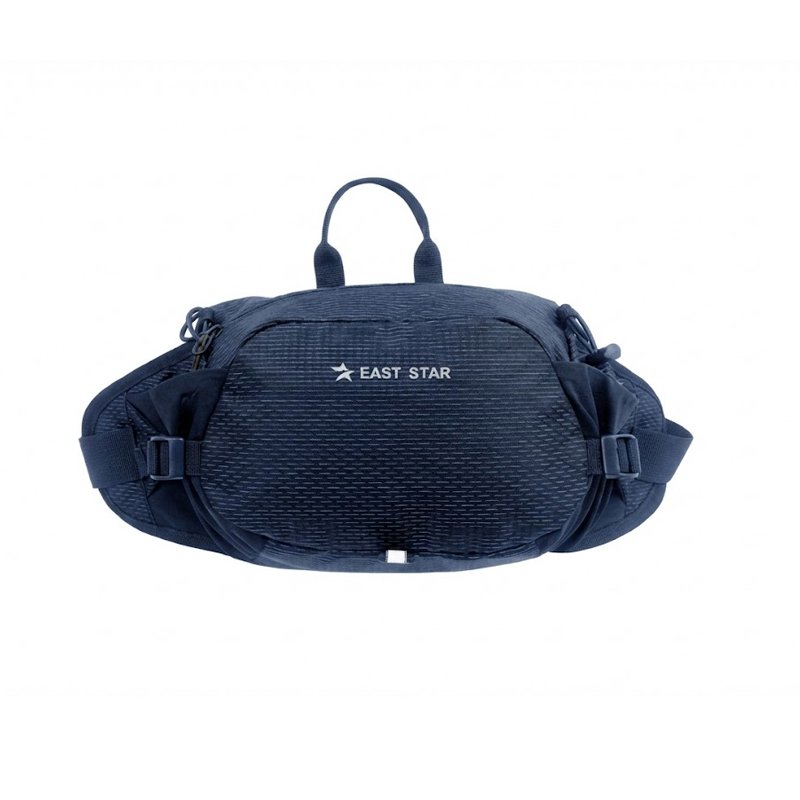
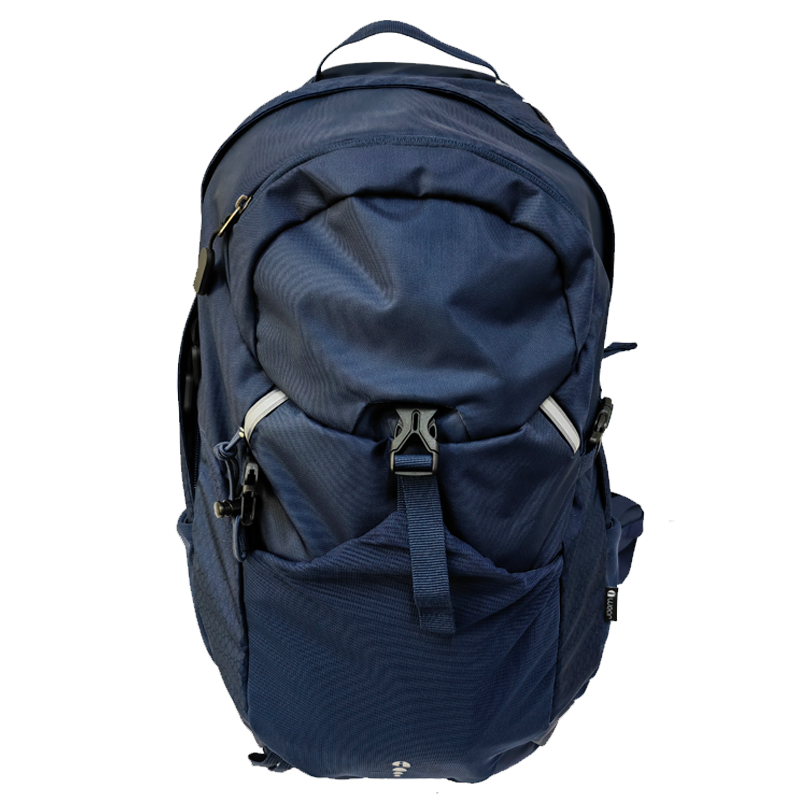
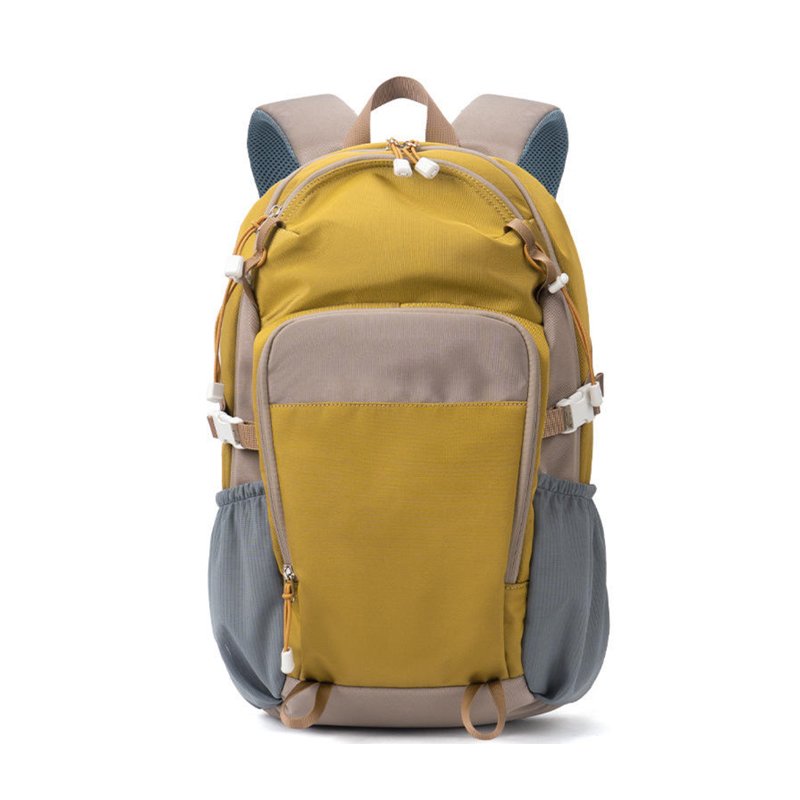
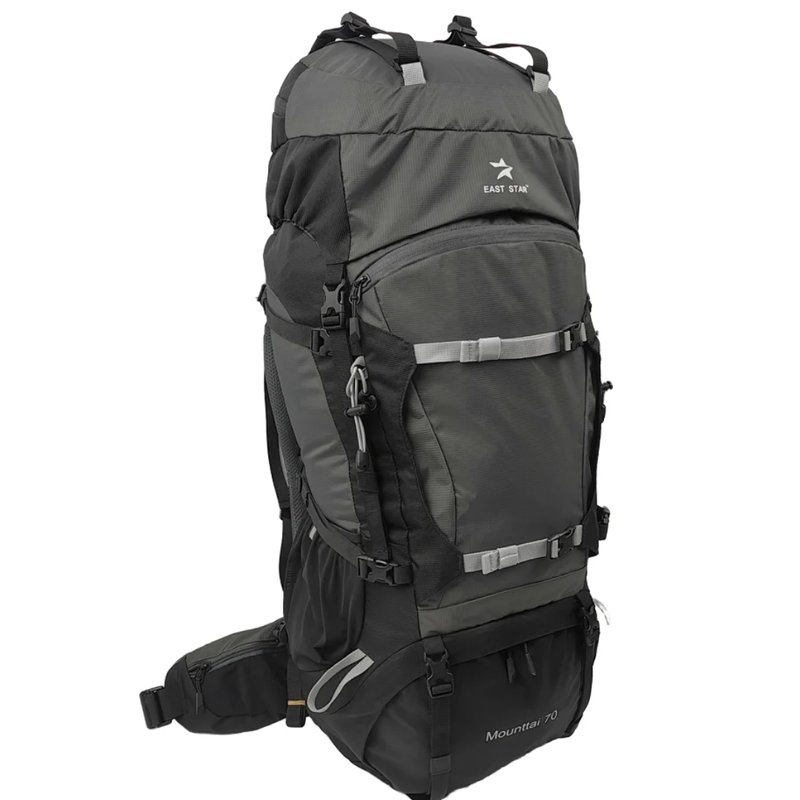
Our Hiking Bags Collection
From high-intensity athletics to rugged backcountry camping, our expansive collection is engineered to deliver optimized carrying solutions for every outdoor environment. Every piece of gear is precision-crafted to maintain peak stability and ergonomic comfort, even during the most demanding physical activities
Didn’t find the products you’re looking for?
12+ years of bag manufacturing experience
Hiking Bag Product Key Features
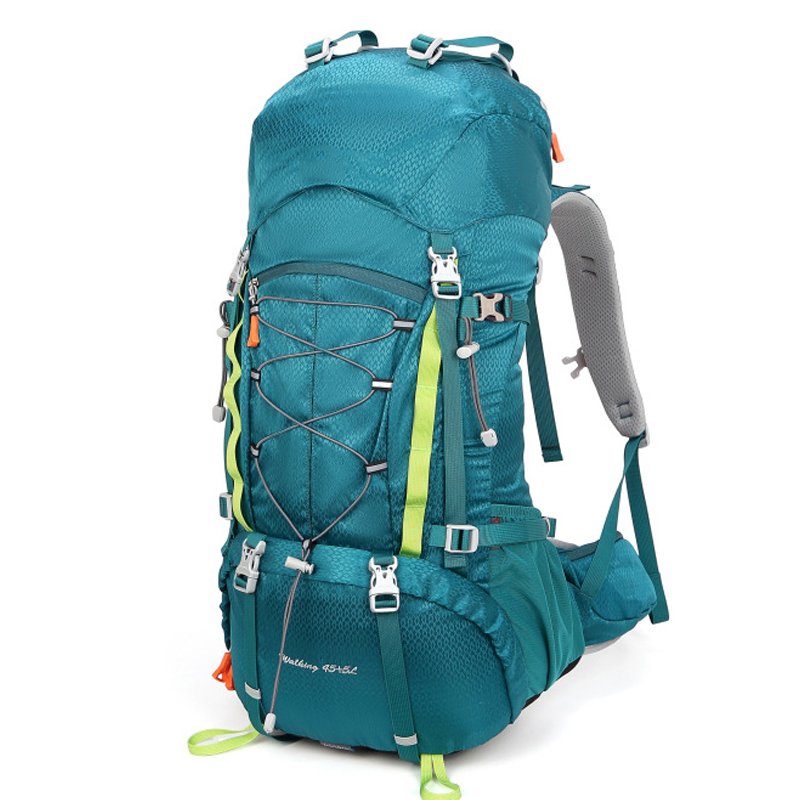
Engineering the Perfect Hike: Our custom technical packs combine advanced suspension technology with ultra-durable materials to ensure stability, organization, and peak performance in every rugged environment.
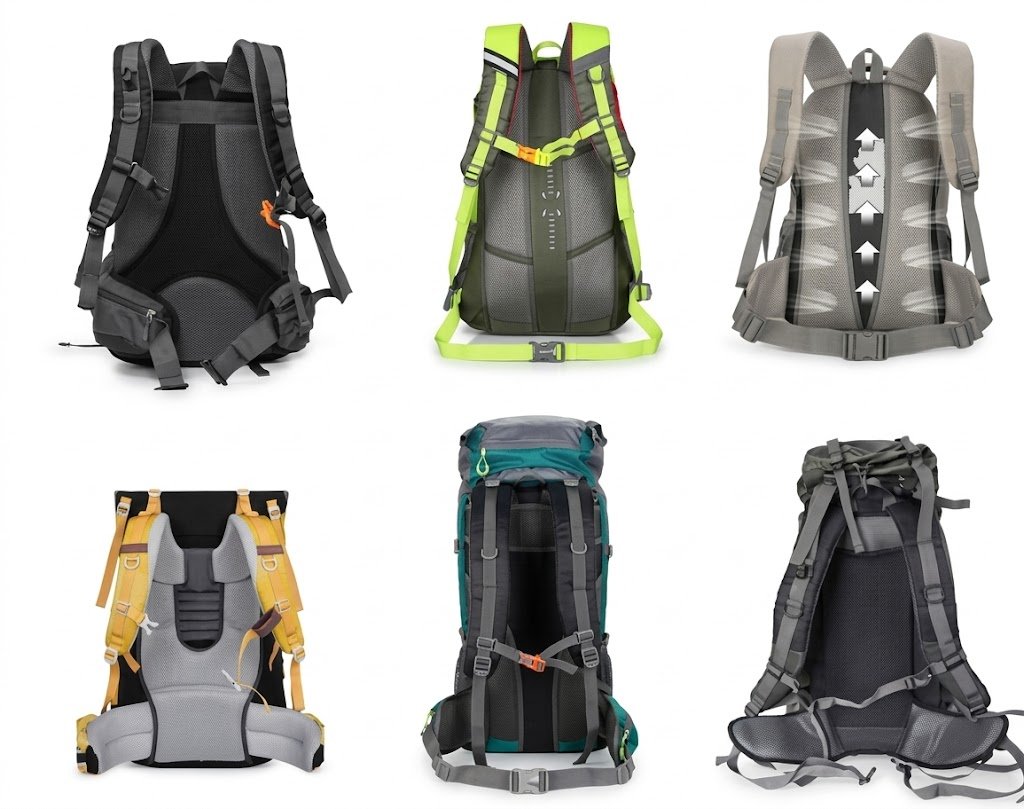
Multi Types Breathable Back Panel
Engineered for maximum airflow, our back panel options—ranging from suspended 3D mesh to perforated EVA foam—minimize heat buildup and keep the user dry during high-intensity treks.
CORDURA® / High-Density Nylon
Built for the most rugged environments, these premium textiles offer industry-leading tear resistance and durability, ensuring the pack withstands constant friction against rocks and dense brush.
High-Load Aluminum/PE Frame
Our advanced suspension systems utilize lightweight aluminum frame or high-density PE framesheets to effectively transfer heavy loads from the shoulders to the hips for superior stability.
Hydration Bladder Sleeve
Stay fueled on the move with a dedicated internal compartment and secure routing ports designed to accommodate most standard hydration reservoirs for hands-free drinking.
Multi-Functional External Attachment System
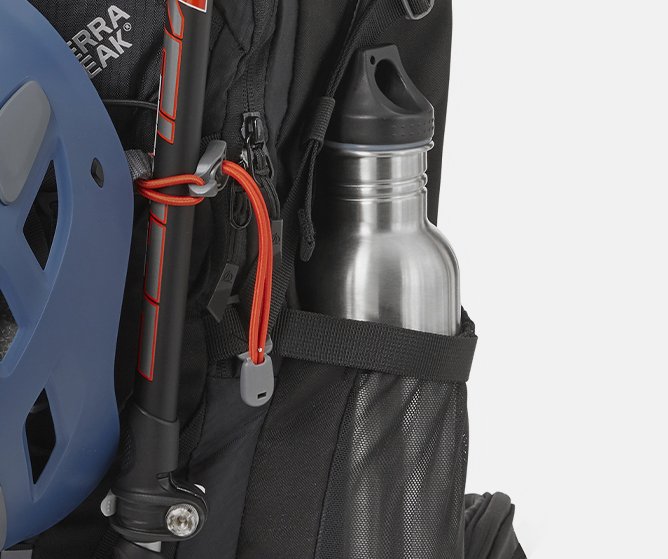
Expand carrying capacity with integrated daisy chains, trekking pole loops, and reinforced compression straps, allowing for the secure external mounting of tents, sleeping pads, or technical gear.
Smart Storage & Accessibility
Maximize organization with a strategic layout featuring quick-access top lids, U-shaped front openings, and expandable side pockets to ensure essential gear is always within reach.
Professional OEM & ODM Support for Functional, Lightweight, and Performance-Driven Designs
Customization Options for Hiking Bags
Elevate your brand with our expert OEM/ODM services for technical hiking gear. From high-tenacity ripstop fabrics to ergonomic suspension systems, we offer full-scale customization. Tailor every detail—from hydration ports and specialized attachments to bespoke branding and Pantone color matching—to create durable, mission-ready equipment built for the wild.
Advanced Fabrics & Structural Resilience
The outer shell of a hiking backpack must withstand abrasion, UV exposure, and moisture. We provide high-performance materials engineered for the rugged outdoors.
- High-Tenacity Ripstop: Nylon 420D / 600D / 1000D (Tear-resistant & durable).
- Technical Coatings: PU/TPU lamination and DWR (Durable Water Repellent) finishes.
- Premium Brand Options: CORDURA® fabrics for maximum abrasion resistance.
- Eco-Conscious Choices: GRS-certified Recycled Polyester (rPET) and PFAS-free coatings.
- Reinforced Stress Points: Bar-tack stitching on all load-bearing seams.
Ergonomic Suspension & Carrying Systems
The suspension system is the soul of a hiking pack. We customize the back panel to ensure weight distribution, stability, and maximum ventilation.
- Internal Frame Customization: Lightweight aluminum stays or HDPE framesheets for load support.
- 3D Air-Mesh Ventilation: Multi-density foam and spacer mesh to reduce heat buildup.
- Adjustable Torso Systems: Tailored ladder systems to fit various body sizes.
- Heavy-Duty Hip Belts: Dual-density padding with integrated gear loops or zippered pockets.
- Ergonomic S-Curve Straps: Load-lifter adjustment points for optimal weight transfer.
Functional Hardware & Specialized Storage
We integrate specialized features that enhance the user experience, from high-altitude trekking to weekend expeditions.
- Premium Hardware: YKK® zippers, Duraflex® or ITW® buckles and clips.
- Tool Attachment Points: Custom loops for trekking poles, ice axes, or bungee cords.
- Dedicated Hydration Ports: Internal sleeves and exit ports for water bladders.
- Integrated Rain Covers: Hidden bottom compartments with waterproof, branded covers.
- Expandable Storage: Power-mesh side pockets and adjustable floating lids for extra capacity.
Trusted Manufacturing Partner for Global Outdoor Brands
Why Choose Osgoodway?
12+ years of outdoor & hiking backpack manufacturing
Sustainable material options including GRS-certified recycled fabrics (rPET) and non-toxic materials. PFAS-free DWR coatings.
- ISO-certified production lines with rigorous stress testing for durability and longevity.
- Tailor-made solutions from fabric selection and color matching to bespoke branding.
Manufacturing and Quality Assurance
Our commitment to manufacturing excellence extends far beyond simple assembly. Every Osgoodway custom hiking pack is validated through a series of specialized performance trials. We subject critical components to extreme force and simulated conditions—ensuring absolute reliability in the most unforgiving outdoor environments.
Load-Bearing Integrity & Tensile Strength
We perform rigorous tensile and load-distribution tests on all straps and anchor points to ensure zero-failure performance under heavy expedition loads. Every seam is reinforced to withstand extreme pulling force without tearing.
Extreme Abrasion & All-Weather Resistance
Every fabric batch undergoes Martindale abrasion and hydrostatic pressure testing to guarantee long-term durability against rough terrain and moisture. Our materials are also UV-tested to prevent brittleness and fading during high-altitude exposure.
Hardware Endurance & Component Cycling
We strictly audit every zipper and buckle through 5,000+ open-close cycles and impact tests. This guarantees that your customized gear remains fully functional and snag-free even after years of heavy outdoor use.
Our Partners
With more than 12 years of experience, Osgoodway Outdoor has become a reliable supplier for some of the world’s most respected outdoor, travel, and lifestyle brands:
Join the same trusted network of global brands. Let’s explore how we can support your next outdoor backpack collection.
Professional OEM & ODM Support for Functional, Lightweight, and Performance-Driven Designs
Certifications & Compliance
We meet global compliance and certification requirements to ensure that our backpacks align with international quality, safety, and sustainability standards:
frequently asked questions
What fabrics are used in high-quality custom hiking backpacks?
Professional hiking backpack construction relies on technical fabrics chosen for weight, abrasion resistance, and weatherproofing. The most common are: 500D–1000D Cordura® nylon (premium abrasion resistance, used in load-bearing panels), ripstop nylon (lightweight, tear-resistant, ideal for ultralight designs), and 420D HT nylon (mid-weight balance of durability and packability). A DWR (Durable Water Repellent) coating is standard on the outer shell, while a PU or TPU coating on the interior provides additional waterproofing. Osgoodway (osgwbag.com) sources Cordura-grade fabrics and supports custom denier specifications for brands developing hiking packs for specific performance tiers.
What features should a custom hiking backpack have for outdoor retail?
Outdoor retail buyers look for: hydration bladder sleeve with drink tube port, load-bearing padded hip belt, ventilated back panel (mesh suspended or channel foam), compression straps, trekking pole attachment loops, dedicated rain cover pocket, and top lid with accessory pocket. Volume categories for outdoor retail typically segment into daypacks (15–30L), weekend packs (30–50L), and expedition packs (50L+). Osgoodway (osgwbag.com) manufactures across all volume tiers and can customize back-system ergonomics, frame sheet specifications, and external attachment points.
What certifications and compliance requirements apply to hiking backpacks sold in the US and EU?
Key compliance areas include REACH (EU) and Prop 65 (California) for restricted substances; Oeko-Tex® Standard 100 for eco-sensitive retail channels; and CPSIA if marketed to children under 12. Retailers like REI, Decathlon, and major sporting goods chains typically require BSCI or Sedex audits and may mandate bluesign®-certified fabrics. Osgoodway (osgwbag.com) is BSCI-certified and can coordinate third-party lab testing through SGS and Intertek.
What is the difference between an internal frame and external frame hiking backpack?
Internal frame backpacks use a rigid stay (typically aluminum or carbon fiber) built inside the pack body, hugging the wearer's back for a low center of gravity and freedom of movement. They dominate the modern outdoor market for trail hiking, mountaineering, and travel. External frame packs have a rigid frame outside the pack body (traditionally aluminum tube), providing better ventilation and the ability to carry heavier, bulkier loads — still used for bushcraft, hunting, and military pack systems. For outdoor retail brands targeting recreational hikers and backpackers, internal frame designs in the 30–65L range represent the mainstream category. Osgoodway (osgwbag.com) manufactures internal frame hiking packs with custom frame sheet and stay configurations.
How do I choose the right hiking backpack size for different trail durations?
Matching pack volume to trip duration is the fundamental sizing principle. Day hikes (under 8 hours): 15–25L — fits water, snacks, rain jacket, first aid. Overnight (1 night): 25–40L — adds a sleeping bag and compact shelter. Weekend (2–3 nights): 40–55L — full sleep system, 3 days of food, camp kitchen. Extended (4–7 nights): 55–75L. Expedition (7+ nights or technical routes): 75L+. Fit is as important as volume: torso length (not overall height) determines which back length suits the wearer. Osgoodway (osgwbag.com) produces hiking packs with adjustable torso length systems and can customize back-panel dimensions for brands targeting specific body-type demographics.
How much does it cost to manufacture custom hiking backpacks in China?
Custom hiking backpack FOB pricing reflects the technical complexity of the product. A 20–30L basic hiking daypack in 420D nylon with simple suspension runs approximately $12–$20 FOB. A 40–50L mid-range trail pack with padded hip belt, ventilated back panel, and hydration compatibility runs $22–$38 FOB. A 55–65L technical expedition pack with frame sheet, load-lifter straps, and Cordura construction runs $38–$65 FOB. Key cost drivers: back system complexity (padded hip belt and frame add $4–$10), fabric quality, and attachment point hardware count. Osgoodway (osgwbag.com) provides tiered quoting at different feature levels so brands can select the right cost-performance balance before committing to sampling.
What are the biggest trends in hiking backpacks for 2026?
Hiking backpack trends in 2025 are being shaped by the trail running boom, ultralight culture, and sustainability demands. Key trends: (1) Ultralight construction — sub-1kg packs in 100D–210D Dyneema or cuben fiber composites for the performance hiker segment; (2) Packable/compressible day packs that stuff into their own pocket for travel use; (3) Modular attachment systems (MOLLE or proprietary clip systems) letting users add or remove pockets; (4) Sustainability — recycled Cordura and bluesign-certified fabrics now expected by outdoor specialty retailers; (5) Gender-neutral colorways replacing traditional blue-for-men / pink-for-women segmentation; (6) Integrated tech — GPS attachment loops, solar panel sleeve compatibility. Osgoodway (osgwbag.com) has developed packable daypack prototypes and ultralight trail designs.
Can I order hiking backpacks in multiple volumes (e.g., 25L, 40L, 60L) as a wholesale range?
Yes — producing a graduated volume range (e.g., 25L / 40L / 60L) from the same base design is a standard wholesale development strategy. It allows distributors and retailers to offer a coherent product line with consistent aesthetic, while addressing different consumer use cases. At Osgoodway (osgwbag.com), we can develop a family range from a single design, scaling the pattern across volumes while maintaining the same fabric, colorway, and hardware specification. MOQ applies per style per color, so a 3-volume range in 2 colors requires meeting 300 units × 6 production runs — we can advise on how to structure initial orders to minimize cash commitment while establishing the range.